 EN
The Failure Point Is Almost Never the Face
Most moisture damage in built environments does not start on the visible surface. It starts at a cut edge, a drilled hole, a seam, or a junction where one material meets another. A laminate-faced MDF board can carry a perfectly water-resistant decorative skin and still fail within a season because the core behind that skin is engineered wood fiber, and wood fiber moves when it takes on water. The cut edge at the bottom of a door, the unsealed penetration around a pipe, the joint where a panel meets a wet floor: those are the places where moisture finds its way in and the panel loses its shape from the inside out.
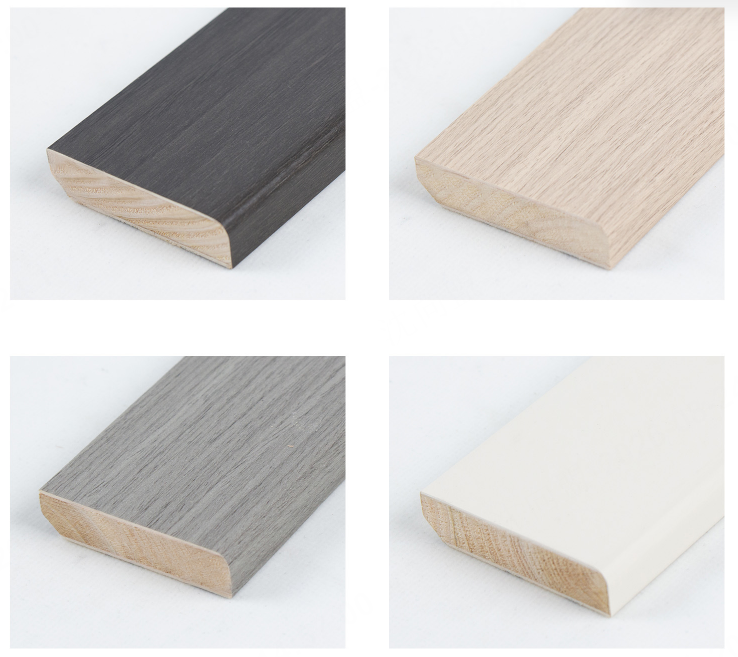
That is the context in which compact laminate earns its reputation. The material is not a coated board. It is a solid phenolic panel built from layers of kraft paper impregnated with thermosetting resin, consolidated under heat and pressure into a homogeneous, non-porous sheet. There is no separate substrate. When the panel is machined, the exposed edge is still laminate through its full thickness. Water has nowhere to wick into because there is no fibrous core waiting behind the face.
Why Phenolic Chemistry Beats a Coating Strategy
Phenolic resins are chosen for this application because their cured structure is dense, hydrophobic, and dimensionally stable across a wide range of moisture and temperature conditions. The resin saturates the paper layers rather than sitting on top of them. A decorative melamine surface, where present, sits above a core that is already moisture-resistant, so the panel does not depend on a thin film to keep water out. The protection runs through the section.
This chemistry has a practical consequence for how the material behaves after fabrication. A coated panel depends on edge sealing to survive. A compact laminate panel does not depend on edge banding or sealant to maintain its integrity at a cut. Cable openings, routed grooves, and exposed machined edges remain part of the same consolidated laminate. That makes the material suitable for the places where moisture control is hardest to guarantee: shower partitions, locker carcasses in changing rooms, laboratory casework, and washdown environments where standing water is a normal condition rather than an accident.
The Test Data That Separates Performance Claims from Performance
European standard EN 438-2 provides the benchmark tests that matter here, and the numbers from published technical data sheets are worth reading closely. Boiling water immersion is the most aggressive accelerated test in the standard suite. Formica’s compact grade data lists mass increase of 1.0 percent and thickness swelling of 0.06 percent after boiling water exposure, with a moisture resistance rating of 5 on the EN 438-2 test method 27 scale. Steam resistance and crazing resistance both sit at rating 5. Other published compact laminate values put thickness swelling after boiling water immersion at or below 2 percent, and typical values in manufacturer data sit well under that ceiling.
| Property | Compact laminate (published range) | HPL-faced MDF | What the difference means in service |
|---|---|---|---|
| Core construction | Solid phenolic-impregnated kraft layers | Wood fiber core with laminated face | No fibrous substrate to swell or delaminate |
| Boiling water thickness change | Roughly 0.06 percent to under 2 percent depending on grade | Face resists, core vulnerable at cut edges | Machined edges and penetrations stay stable |
| Moisture resistance rating (EN 438-2 method 27) | Rating 5 | Not applicable to exposed core | Performance holds at exposed sections, not just faces |
| Edge treatment requirement | None for moisture integrity | Edge band or sealant required | Fewer failure points in wet areas |
| Self-supporting capability | Yes, above a thickness threshold depending on span and load | Requires continuous substrate | Simplifies wet-area construction and detailing |
The honest caveat is that compact laminate is not a waterproof membrane in the same sense as a fully sealed tanking system. It is a moisture-resistant panel, not a substitute for building envelope waterproofing. Joints between panels still need appropriate sealant or profile design, and standing water should drain rather than pool. The material raises the tolerance for moisture exposure considerably. It does not eliminate the need for competent wet-area detailing.
Where the Material Proves Itself: Wet-Area Case Evidence
The applications where compact laminate has displaced other materials most decisively are those where moisture is continuous and cleaning is aggressive. In a military barracks refurbishment in Victoria, Australia, compact laminate was specified for full-height shower and toilet partitions, lockers, and bench seating in communal change rooms. The brief called for systems suitable for wet areas, and the installed product was a water-resistant compact grade rather than a substrate-based board. The specification was driven by the same logic that governs hospital and aquatic centre work: surfaces that see water, disinfectant, and heavy use every day need a section that does not depend on a vulnerable core.
Healthcare projects follow the same pattern. Large hospital installations have used compact laminate for toilet cubicle partitions, shower systems, and wall cladding in patient areas, with hygiene and moisture exposure as the deciding criteria. Published case documentation from hospital projects notes phenolic compact as an ideal material for sanitary facilities because of its hygienic behavior and moisture stability. The common thread across these projects is not aesthetic preference. It is a calculation about lifecycle disruption: replacing swollen or delaminated partitions in an operating facility is far more expensive than specifying a panel that does not depend on edge protection to survive.
The Specification Details That Decide Whether the Panel Lives Up to Its Chemistry
Compact laminate is not a specification you can write with a single line item. Thickness has to match the span and the loading. A panel that is self-supporting at one span may need intermediate support at a longer one. The material is available in a wide thickness range, and published flexural data gives the designer the numbers to check. Joint design matters as much as panel chemistry. Panel-to-panel joints in a shower environment need a profile or sealant strategy that accommodates minor movement without creating a water trap. Wall junctions and floor junctions need the same attention.
There is also a fabrication dimension that separates experienced suppliers from catalog vendors. Compact laminate can be routed, drilled, and machined without edge banding, but the tooling and the feed rates matter for a clean edge. Poorly machined edges create a place for soil and moisture to accumulate even on a solid phenolic panel. The manufacturing discipline behind the panel is as important as the resin system inside it. Andiwilson approaches compact laminate production with core consolidation and machining consistency treated as the foundation of the product, keeping the phenolic layup, pressing, and finishing inside a coordinated manufacturing flow rather than treating the panel as a commodity sheet. For high-moisture environments, that consistency is what turns a good material specification into an installation that still performs years after the handover.